RE-ROPES
Lift Belt Supply & Replacement
Coated steel belt survey, supply and replacement for Otis Gen2, Schindler and Elatech lift systems. Independent supply and fit across the UK and Ireland since 1986.
Overview
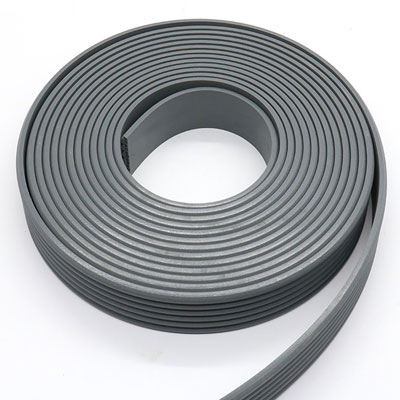
Since Otis introduced the Gen2 system in 2000, polyurethane-coated steel belts have replaced conventional traction ropes in a large share of modern lifts. A coated steel belt carries the car and counterweight on flat bands of high-tensile steel cords sealed inside a polyurethane jacket. Otis states the design is stronger and more flexible than round rope, runs on a substantially smaller sheave, never requires lubrication, and removes the metal-to-metal contact that makes rope-driven lifts noisy.
That flexibility changes how the suspension system has to be maintained. A coated steel belt cannot be assessed by counting broken wires the way a wire rope can. Belts are manufacturer-specific, are normally replaced as a complete matched set rather than one at a time, and depend on the terminations, sheaves and connectors being right as well. Specifying the wrong belt means a lift that will not run — or one that will not satisfy its next thorough examination.
Re-Ropes supplies and fits OEM-approved lift belts for Gen2 and comparable belt-driven traction systems, together with the connectors, pulleys and specialist belt-cleaning products that go with them. We were the first company in the UK to provide an independent supply-and-fit service to the lift industry, and we have been re-roping lifts since 1986. Our engineers work across the UK and the Republic of Ireland from depots including London (Erith), Belfast and Dublin, with belt sets, terminations and ancillaries held in stock.
What the Service Includes
- OEM-approved belt supply — coated steel belt sets for Otis Gen2, Schindler and Elatech systems, matched to the original manufacturer’s specification and part reference.
- Belt condition survey and wear assessment — on-site inspection of jacket condition, cord exposure, running-face wear, tension across the set and termination condition, recorded in a written report.
- Complete belt-set replacement — removal of the existing belts and installation of the new set by engineers experienced in belt-driven traction systems.
- Terminations, connectors and end fasteners — supply and fitting of the compatible hitch and connector components. A belt set is only as good as its terminations.
- Traction sheave and diverter pulley work — inspection, re-grooving and refurbishment where the running surface has worn, so a new belt set is not run onto a worn sheave. Lift Repair & Refurbishment – WH Scott Group
- Belt tension setting and equalisation — tension checked and equalised across the set, then proved under load.
- Specialist belt cleaning products — approved cleaning systems that remove contamination without attacking the polyurethane jacket.
- Technical compatibility guidance — belt type, width, length, load family, suspension arrangement and system requirements confirmed before anything is ordered.
- Certification and documentation — belt certificates and client-specific paperwork issued on completion, ready for your maintenance and thorough-examination records.
- Planned works scheduling — replacement planned around building occupancy and access to limit time out of service.
Scope & Equipment
- Polyurethane-coated steel belts — also called coated steel belts, CSBs or flat suspension belts — used in modern traction and machine-room-less lifts
- Otis Gen2 and later Otis belt-driven platforms, and equivalent belt-driven systems from other manufacturers
- Associated components: terminations and connectors, traction sheaves, diverter pulleys, and belt-cleaning systems
- Schindler and Elatech belt configurations
- Passenger, goods-passenger and goods lifts in commercial, residential, public-sector and infrastructure buildings
- Legacy and current lift systems, in occupied buildings and as part of planned refurbishment programmes
Our Process
Survey, specify, supply, fit, guarantee — the process Re-Ropes has worked to since 1986, applied to belt-driven systems
- Survey. An engineer attends site to identify the lift system, belt type and OEM part reference, measure the existing belts and terminations, and assess the condition of sheaves, diverter pulleys and connectors.
- Specify & report. You receive a written report and quotation setting out the belt specification, the components required, and any sheave or termination work needed before the new belts go on.
- Supply. OEM-approved belts, connectors and ancillaries supplied to the confirmed specification, from stock where the item is held.
- Prepare. Access, isolation and working arrangements agreed with the building owner and lift owner, and the works sequenced to limit time out of service.
- Fit. Existing belts removed and the new set installed, terminated and tensioned by engineers working to the manufacturer’s requirements and to recognised safe working practice for lifts.
- Verify & guarantee. Alignment, tension and operation checked, the lift proved under load, certificates and client paperwork issued, and the work guaranteed.
Certifications & Standards
- LOLER 1998 — Lifting Operations and Lifting Equipment Regulations. Thorough examination of lifts used at work: at least six-monthly where the lift carries persons, at least twelve-monthly for goods-only lifts, with a Schedule 1 report.
- PUWER 1998 — Provision and Use of Work Equipment Regulations: suitability, maintenance and safe use of work equipment.
- S.I. No. 299 of 2007 — the equivalent statutory regime in the Republic of Ireland.
- BS EN 81-20 and BS EN 81-50 — the safety standards to which modern passenger and goods-passenger lifts are constructed, and to which their safety components are designed, calculated, examined and tested.
- BS 7255:2023 — Safe working on lifts, code of practice. The recognised UK code for working safely on lift installations.
- OEM requirements — belt type, part reference, load family, tension and installation method as specified by the original equipment manufacturer. Sector guidance on Otis Gen2 coated steel belts is also published by SAFed.
- Group certification — ISO 9001, ISO 14001, ISO 45001 and ISO 27001 certified management systems; LEEA membership for inspection and thorough examination of lifting equipment.
Related Services
Lift Rope Supply & Installation
Lift rope supply and installation services for elevators, cranes, and lifting systems, delivered through a structured survey, supply, fit, and guarantee approach to ensure safe operation and compliance.
Lift Repair & Refurbishment
Lift repair and refurbishment services covering motors, gearboxes, brakes, sheaves, and safety-critical components, delivered with rapid turnaround to minimise lift downtime and restore equipment to manufacturer specification.
Lift Technical Services
Lift technical services provide specialist engineering support, inspection, and advisory solutions for lift ropes and associated systems, ensuring safe operation, compliance, and performance optimisation across lift installations.
Frequently Asked Questions
What is a lift belt, and how does it differ from a traditional wire rope?
A lift belt — properly a coated steel belt — is a flat band of high-tensile steel cords sealed inside a polyurethane jacket, used in place of round steel wire rope to suspend the car and counterweight. Compared with wire rope it is more flexible, runs on a much smaller traction sheave, needs no lubrication, and runs more quietly because there is no metal-to-metal contact.
Which lift systems use belts instead of ropes?
The Otis Gen2 system, introduced in 2000, and later Otis belt-driven platforms use flat coated steel belts, as do comparable machine-room-less designs from other manufacturers, including Schindler. If you can see flat bands rather than round ropes at the traction sheave, your lift is belt-driven.
Can you supply OEM-approved lift belts?
Yes. We supply OEM-approved belts from manufacturers including Otis, Schindler and Elatech, together with compatible connectors, pulleys and cleaning products, so compatibility and compliance with the original system specification are preserved.
How often should lift belts be replaced?
There is no fixed interval. Replacement is driven by condition, duty cycle, environment and the manufacturer’s guidance, established through regular inspection and, where fitted, belt monitoring data. What matters is that belt condition is being assessed — not that a particular number of years has passed.
How long do coated steel belts last?
Service life varies widely with traffic, load, travel and environment, so we will not publish a single figure. A high-traffic lift in a dusty or humid environment will reach the end of belt life considerably sooner than a lightly used one. A survey against the manufacturer’s criteria will tell you where your belts actually are.
Can an independent company replace Otis Gen2 belts, or must the original installer do it?
You are generally free to obtain independent quotations for belt supply and replacement, provided OEM-approved components are fitted to the original specification by competent engineers and the work is properly documented. Re-Ropes was the first company in the UK to offer an independent supply-and-fit service to the lift industry, and has done so since 1986.
How do I know if my lift belts need replacing?
The indicators are damage or degradation of the polyurethane jacket, exposed or broken steel cords, uneven wear across the set or to the ribbed running face, tension differential between belts, elongation beyond the manufacturer’s limits, and worn terminations or sheave grooves. A belt monitoring warning, or a defect noted on a thorough examination report, should also trigger a survey.
My lift’s belt monitoring system has flagged a warning. What happens next?
Treat it as the start of a planned replacement rather than a breakdown. A monitoring indication typically gives you time to have the belts surveyed, obtain a specification and quotation, agree a budget and schedule the work around the building — which is a far better position than a lift that has already stopped.
Are lift belts covered by LOLER thorough examination?
Yes. Lifts used at work require thorough examination under LOLER 1998 — at least six-monthly where the lift carries people, at least twelve-monthly for goods-only lifts — and the condition of the suspension media, belts included, is central to that examination. Any defect recorded must be actioned within the timescale stated in the report.
Get in Touch
Tell Us About Your Project
Whether you need a single piece of equipment or a fully engineered lifting system, our specialists can help. Tell us your load, environment and compliance requirements — we’ll do the rest.